Introdução: The Unseen Dangers of Tool Mismanagement
Every year, the aviation industry loses millions of euros to foreign object debris (FOD) incidents, many of which originate from unaccounted maintenance tools. A forgotten spanner inside an engine nacelle or a missing socket left in a flight control compartment can lead to catastrophic failures. For European MROs, the regulatory framework demands absolute tool control. EASA Part-145.A.45 explicitly requires that organisations have procedures to ensure all tools are accounted for after completion of maintenance. Traditional manual logging and shadow boards fall short under the pressure of fast-paced operations. RFID technology has emerged as the definitive answer—offering real-time, automated visibility that transforms tool accountability and audit-readiness.
Regulatory Landscape and Market Context
Europe’s aviation MRO sector is one of the world’s largest, projected to reach €40 billion by 2030. Com mais de 6,000 EASA Part-145 approved organisations, competition is intense, and compliance scrutiny is unrelenting. Tool-related FOD accounts for approximately 5% of all reported events, with an average direct cost of €50,000 per incident—and that figure skyrockets when factoring in aircraft downtime and reputational damage. EASA’s growing emphasis on safety management systems (SMS) pushes MROs to adopt digital, auditable tool control methods. RFID systems not only meet these demands but also deliver operational ROI through reduced search time, optimised tool calibration scheduling, and zero paperwork.
Technical Specifications of RFID Tool Tracking
Understanding the technical building blocks is essential for choosing a system that survives the harsh hangar environment. The following table summarises the key components:
| Component | Typical Specification | Why It Matters |
|---|---|---|
| Tags RFID | UHF EPC Gen2v2, ISO 18000 - 6C, often with on-metal design | Tools are mostly metallic; standard labels won’t work. On-metal UHF RFID tags are engineered with ferrite shielding to maintain reliable reads. |
| Frequência | UHF (860–960 MHz) | Provides read ranges up to 8 Metros, ideal for portal scanning of entire toolkits. |
| Leitores | Fixed multi-port readers (4 ou 8 ports) or handheld devices | Fixo RFID reader modules support zone‑based monitoring; handhelds enable spot checks and tool location. |
| Tag Memory | EPC memory (min 96 bits de), memória do usuário (até 512 bits de) | Stores tool serial number, calibration date, and maintenance history directly on the tag. |
| Durabilidade | IP68, chemical‑resistant, operating temperature −40°C to +150°C | Aviation solvents, hydraulic fluids, and steam cleaning can destroy conventional tags. Industrial-grade RFID hard tags are built for these extremes. |
Key Environmental Considerations
European MRO hangars present unique challenges. Tags must resist:
- Chemical exposure: Skydrol, jet fuel, and de-icing fluids can degrade adhesives and plastics.
- Thermal cycling: Tools may move from −30°C ramp conditions to over 120°C during autoclave curing.
- Impact and abrasion: Heavy tool cabinets, drop scenarios, and vibration require robust encapsulation.
Selecting tags with thermoplastic or ceramic enclosures and chemical-resistant bonding ensures longevity. For high-temperature operations, high-temperature RFID tags can withstand up to 250°C, making them suitable for engine maintenance areas.
System Integration and Software Architecture
An RFID tool control system is only as strong as its integration backbone. The typical architecture includes:
- Middleware: Filters and aggregates raw tag reads, processes events according to business rules.
- Database: Central repository linking tag IDs to tool records, calibration schedules, and employee assignments.
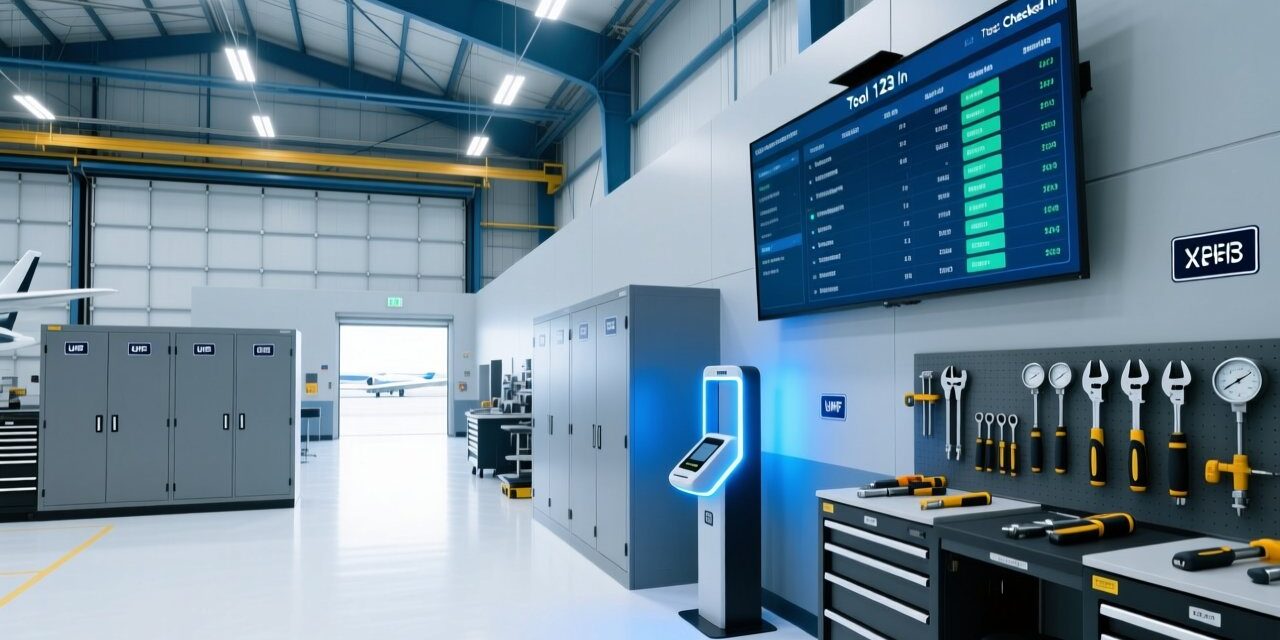
- User Interface: Dashboard displaying real-time tool location, check-in/out status, and automated low-stock alerts.
- API connectors: Enable bidirectional sync with existing MRO software (por exemplo, AMOS, TRAX).
When a mechanic approaches a gate, a fixed reader automatically logs which tools are leaving the workshop. Upon return, the system reconciles the kit contents and instantly flags any discrepancy, while updating the digital audit trail required by EASA. This closed-loop process eliminates manual scanning errors and provides irrefutable compliance records.
Practical Deployment Steps
Successful implementation follows a phased methodology:
1. Tool Inventory Audit and Tag Selection
Catalogue every tool, categorise by material (metal, plástico, composite) and size. Choose tags that match the form factor—embedding RFID chips into small tools may require ultra-small RFID chips; larger items can use bolt-on or cable-tie tags. Perform read-range tests in realistic hangar environments, as reflective surfaces and electromagnetic interference from equipment can affect performance.
2. Reader Network Design
Place fixed readers at choke points (workshop exits, store room doors) to create automated zones. In larger maintenance bays, overhead antennas can monitor entire work areas. For mobile tool cribs, a handheld RFID scanner with Bluetooth connectivity provides flexibility. Ensure all readers are networked and share data with the central MRO tracking platform.
3. Software Customisation and User Training
Configure the software to mirror existing tool control procedures. Set up role-based access, automated calibration reminders, and reporting templates aligned with EASA audit formats. Train mechanics and inspectors on proper tagging processes and system interaction—change management is critical for adoption.
EASA Part-145.A.45 Compliance in Detail
The regulation states: “The organisation shall ensure that all tools, equipment and particularly test equipment…are controlled and calibrated.” RFID-enabled tool management automates compliance by:
- Real-time tool inventory: Always know what is where, preventing unauthorised tool use.
- Complete audit trail: Every tool movement is timestamped and linked to an individual and a work order.
- FOD mitigation: Post-maintenance scans confirm that all tools have been returned before aircraft sign-off.
- Calibration tracking: Tags can store calibration dates; the system alerts when a tool is due, preventing expired equipment from being used.
During an EASA audit, MROs can instantly generate reports showing full tool lineage for any aircraft maintenance event, dramatically reducing audit preparation time and stress.
Selection Tips for European MROs
When evaluating RFID tool tracking solutions, consider:
- Tag read reliability on mixed materials: Demand proof of ≥99.9% read rates on your actual tool sets.
- Reader interoperability: Ensure the selected readers support the GS1 UHF Gen2v2 protocol, essential for future‑proofing.
- Escalabilidade: The system must grow with your operation, from a single hangar to multiple stations across Europe.
- Local support: Choose a vendor with a presence in Europe to guarantee on-site service and compliance updates.
- Integration capability: Verify pre-built connectors for your MRO software suite to avoid costly custom coding.
RFIDHY specialises in delivering end-to-end MRO tracking solutions that encompass tag design, reader hardware, and seamless integration—all aligned with EASA requirements.
Perguntas Freqüentes
Can RFID tags withstand aviation chemicals and high temperatures?
Sim. Specially designed industrial RFID hard tags and high-temperature tags are built with chemical-resistant materials and can operate from −40°C up to 250°C, making them suitable for hangar and engine maintenance environments.
What is the typical read range of UHF RFID on metal tools?
With proper on-metal UHF RFID tags, read ranges of 4 Para 8 metres are achievable using fixed readers. The exact range depends on tag size, reader antenna gain, and environmental factors such as metal shelving. Always perform site surveys to optimise placement.
How does RFID prevent FOD incidents?
RFID automates tool check-out and check-in processes. Before an aircraft is cleared, a final scan verifies that every tool issued for that task has been returned. If any tool is missing, the system instantly alerts the technician and generates a discrepancy report, effectively eliminating the risk of leaving tools inside the aircraft.
Is integration with existing MRO software possible?
Absolutely. Most advanced RFID tool control systems offer APIs and pre-built connectors for major MRO platforms like AMOS, TRAX, and Ramco. This ensures tool data flows seamlessly into your existing maintenance and logistics systems without disrupting workflows.
How does RFID help with EASA Part-145 audits?
RFID systems automatically generate a time-stamped, unalterable log of every tool movement. During an audit, you can retrieve complete tool history for any work order in seconds, demonstrating full compliance with Part-145.A.45. This reduces manual paperwork and gives auditors confidence in your tool control procedures.
Ready to Achieve EASA-Compliant Tool Control?
RFIDHY delivers tailored RFID tool tracking solutions for aviation MROs across Europe. From rugged on-metal tags to integrated reader networks and software, we help you eliminate FOD risk and streamline audit readiness.